EN
 English
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
204V~512V High-Voltage Rack-Mounted Battery
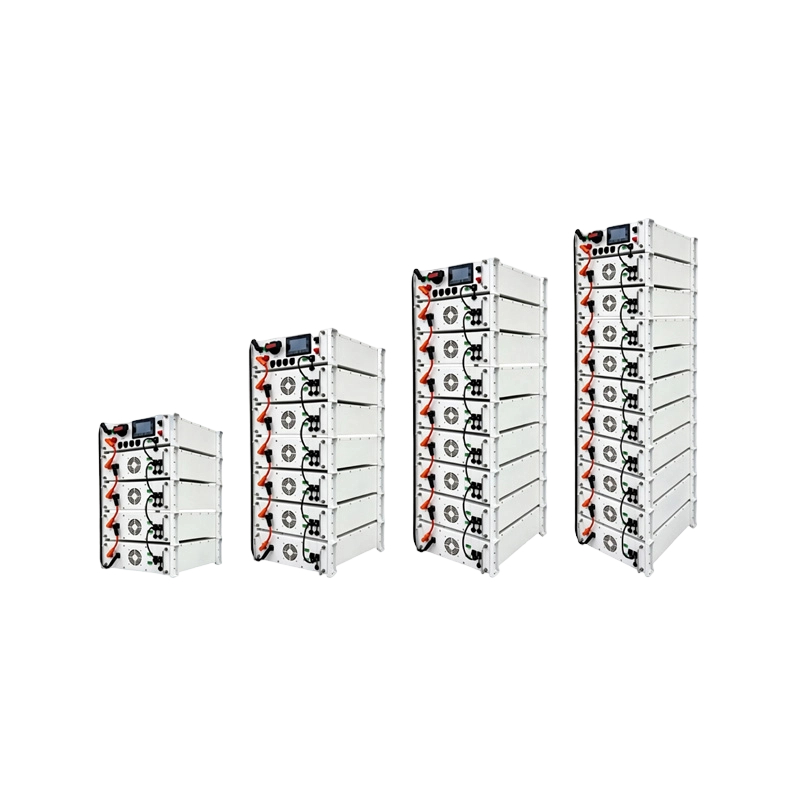
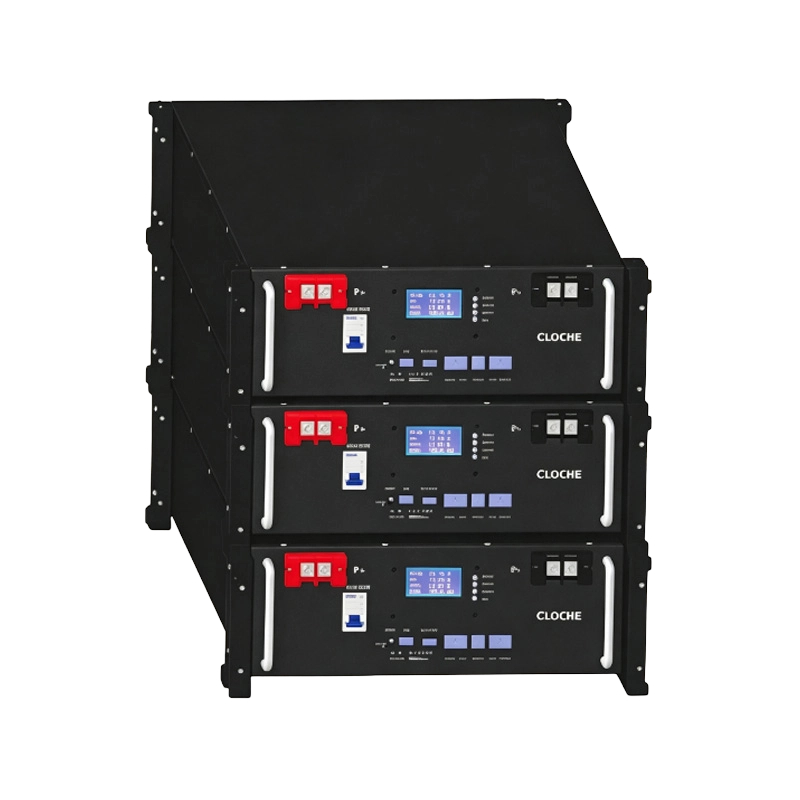
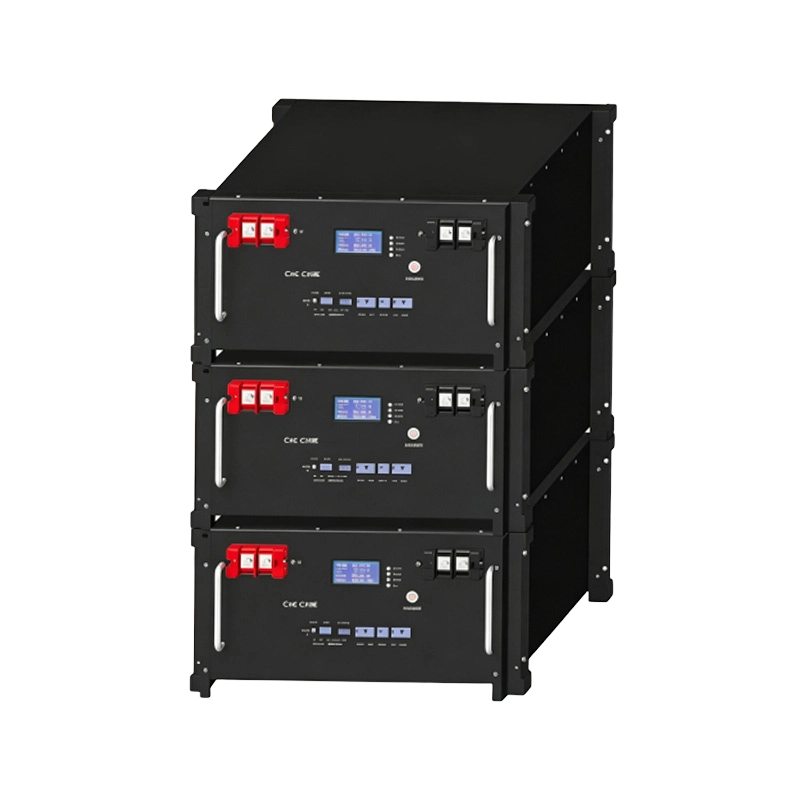
The 204V~512V High-Voltage Rack-Mounted Battery series is a scalable LiFePO4 energy storage system built from 51.2V 100Ah battery modules, delivering 20.48KWh to 51.2KWh of reliable power. This High-Voltage Battery is an ideal solution for commercial & industrial energy storage, data center UPS backup, and large-scale solar integration.
Core Advantages:
1. Modular & Scalable Architecture
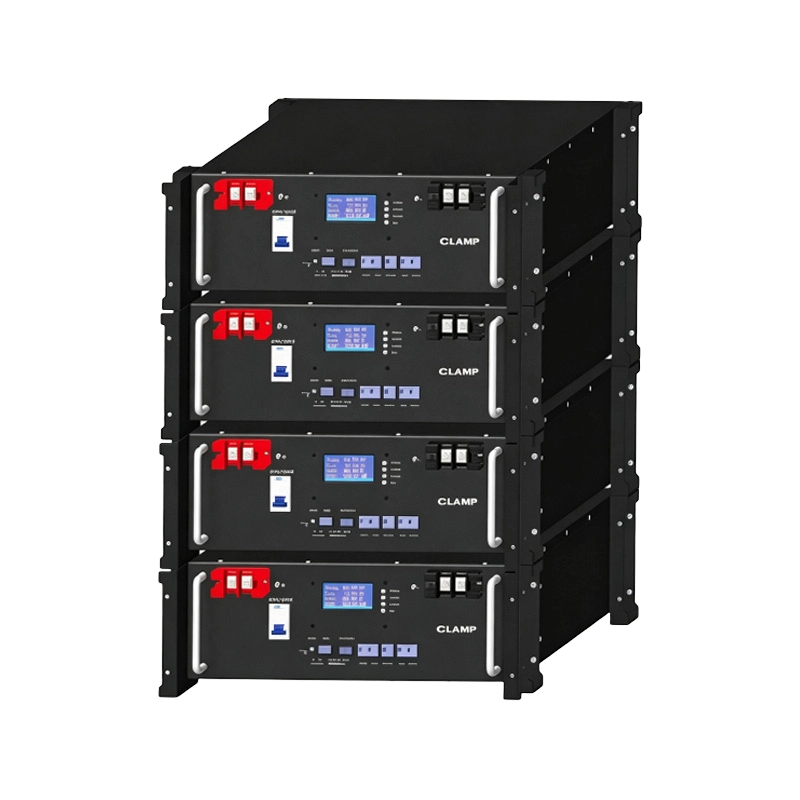
Built from 5.12KWh single modules connected in series, this rack-mounted battery system supports flexible voltage configurations from 204V to 512V. The 4S, 6S, 8S, and 10S options deliver 20.48KWh to 51.2KWh total energy, allowing B2B customers to right-size systems for specific project requirements and scale as energy demands grow.
2. High-Voltage Efficiency
As a High-Voltage Battery, the 512V configuration reduces current levels for a given power output, enabling smaller cable sizes, lower transmission losses, and more efficient inverter operation compared to low-voltage alternatives.
3. Extended Cycle Life
Engineered with Grade A LiFePO4 cells, the 512V Rack Mounted Battery delivers ≥6,000 cycles at 90% DOD while maintaining 70% End of Life capacity. Under standard operating conditions, this translates to over 10 years of reliable daily operation, significantly reducing total cost of ownership for commercial installations.
4. Intelligent Battery Management System (BMS)
The integrated BMS provides comprehensive protection and monitoring:
Overcharge / Over-discharge protection
Overcurrent and short circuit protection
Temperature monitoring and thermal management
Active cell balancing for extended cycle life
Real-time SOC and SOH monitoring
5. Space-Efficient Rack Design
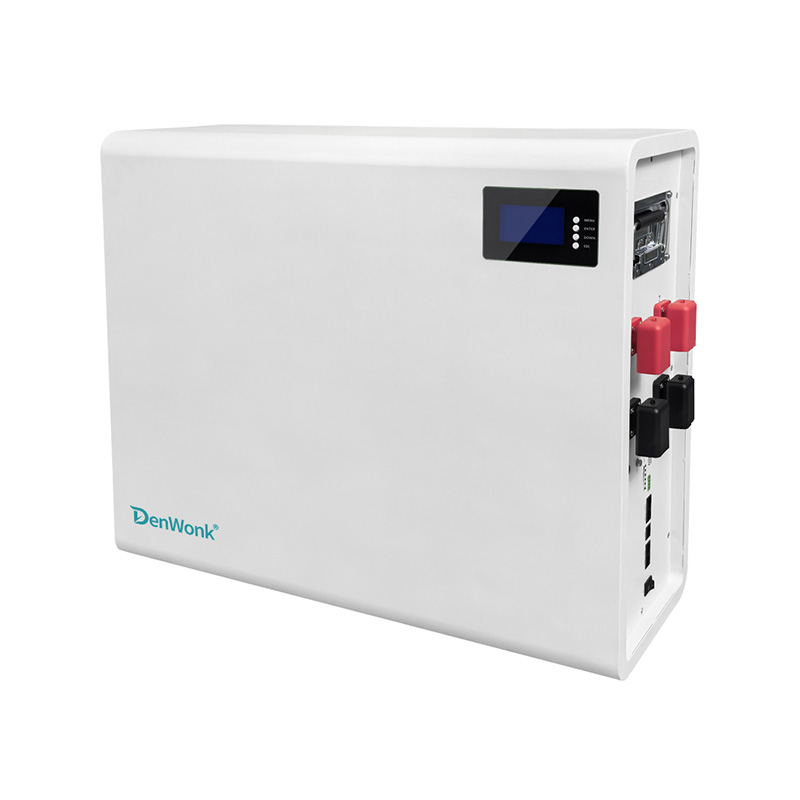
19-inch standard rack mounting with cabinet depth ≥1100mm minimizes footprint while maximizing energy density. The compact 45kg module weight and simple rack installation enable quick deployment and maintenance.
Product Parameters
Application Scenarios
OEM/ODM Services
Solutions
FAQ
| Main Parameter | |||||||
| Cell Model | LC-HR51100-4S | LC-HR51100-6S | LC-HR51100-8S | LC-HR51100-10S | |||
| Capacity(Cell combination method) | 204V100Ah(64S1P) | 307V100Ah(96S1P) | 409V100Ah(128S1P) | 512V100Ah(160S1P) | |||
| Cell Energy(KWh) | 20.48 | 30.72 | 40.96 | 51.2 | |||
| Nominal Voltage(V) | 204.8 | 307.2 | 409.6 | 512 | |||
| Dimension(LW/H,mm) | 590*492*850 | 590*492*1190 | 590*492*1530 | 590*492+1870 | |||
| Weight Approximate(kg) | 208 | 301 | 394 | 487 | |||
| Installation | Simple Rack | ||||||
| Single Battery Module Parameter | |||||||
| Model | LC-HR51100 | ||||||
| Battery Chemistry | LiFePO4 | ||||||
| Capacty(Ah) | 100 | ||||||
| Nominal Voltage(V) | 51.2 | ||||||
| Energy(KWh) | 5.12 | ||||||
| Charge&Discharge Current(A) | 100 | ||||||
| Dimension (LW/H,mm) | 550*442*155 | ||||||
| Weight Approximate(kg) | 45 | ||||||
| IP Rating of enclosure | IP20 | ||||||
| Working Temperature | Charge:0℃~55℃ Discharge:-20℃-55℃ | ||||||
| Cycle Life | ≥6000 cycles(25+2℃,90WDOD,70WEOL) | ||||||
| Installation | 19-inch standard cabinet, cabinet depth ≥1100mm/with rack | ||||||
| Communication Port | CAN2.0,RS485 | ||||||
| Certification | CE-EMC,MSDS,UN38.3 | ||||||
Commercial & Industrial Energy Storage – Peak shaving, load shifting, and demand charge management for businesses and manufacturing facilities
Data Center UPS Backup – High-rate discharge backup power for critical IT infrastructure, distributed data centers, and banking operations
Large-Scale Solar PV Integration – Photovoltaic + storage systems for commercial solar projects and renewable energy optimization
Microgrid & Off-Grid Systems – Reliable power storage for remote industrial sites, telecom infrastructure, and island communities
EV Charging Infrastructure – Buffer storage for fast-charging stations to manage peak demand and reduce grid impact
Industrial Backup Power – Emergency power supply for manufacturing plants, hospitals, and critical facilities
We offer comprehensive OEM/ODM manufacturing capabilities for this High-Voltage Battery platform:
Custom branding (logo, silk-screen, labels, laser engraving)
Tailored BMS parameters and communication protocols
Custom voltage and capacity configurations
Modified enclosure designs and dimensions
Private label packaging and documentation
Dedicated technical support and project consultation
1. Energy Storage System Integrators
We supply standardized rack-mounted battery modules with CAN/RS485 communication protocols, pre-validated for compatibility with major inverter brands. This helps integrators shorten system commissioning cycles and reduce integration costs.
2. EPC Contractors
The 512V Rack Mounted Battery features a modular rack-mounted design with simple installation and rapid parallel/series expansion. We provide complete installation manuals, communication configuration guides, and technical support to assist EPC teams in efficient project delivery.
3. Data Center & UPS System Providers
For mission-critical backup power applications, the High-Voltage Battery series offers high-rate discharge capability, wide voltage range compatibility (204V~512V), and dual-redundancy protection for maximum reliability.
4. Wholesalers and Distributors
This Rack Mounted Battery holds CE-EMC, MSDS, and UN38.3 certifications, delivers ≥6,000 cycle life, and comes with a 5-year warranty. We offer stable supply capacity, flexible delivery schedules, and competitive factory-direct pricing.
5. Commercial Solar Project Developers
By combining solar PV with this High-Voltage Battery storage system, developers can deliver turnkey commercial energy solutions with optimized ROI through peak shaving and time-of-use arbitrage.
Q1: What is the full product specification of this 204V~512V High-Voltage Rack-Mounted Battery series?
This is a series of High-Voltage Rack-Mounted Batteries built from 51.2V 100Ah LiFePO4 modules, offering configurations from 204V/20.48KWh (4S) to 512V/51.2KWh (10S). Each system features 100A charge/discharge current, CAN2.0/RS485 communication, and ≥6,000 cycle life at 90% DOD.
Q2: How many battery modules are required for each configuration?
The 4S configuration uses 4 modules (204V), 6S uses 6 modules (307V), 8S uses 8 modules (409V), and 10S uses 10 modules (512V). Each module is 51.2V/5.12KWh.
Q3: Which inverters are compatible with this Rack Mounted Battery?
The battery supports CAN2.0 and RS485 communication protocols, ensuring compatibility with major inverter brands including Deye, Growatt, Victron, GoodWe, and Sungrow.
Q4: What is the expected cycle life of the 512V Rack Mounted Battery?
≥6,000 cycles at 90% DOD with 70% End of Life capacity retention under standard test conditions (25°C).
Q5: Do you offer OEM/ODM services for this High-Voltage Battery?
Yes, we provide full customization including branding, BMS parameter tuning, connector types, packaging, and more to meet specific project requirements.
Q6: What certifications does this product hold?
The product is certified with CE-EMC, MSDS, and UN38.3 for transportation safety and international compliance.
-
0 m²
Land Area
-
0+
Industry Experience
-
0+
Number of Employees
OUR STORY
Become a World-Class Green Energy Enterprise, Build Low-Carbon Future
Kingway(Jinhua) Display Co., Ltd., a subsidiary of Kingway Group, is a high-tech enterprise focusing on the R&D, manufacturing, sales, and solution provision of new energy storage products. Headquartered in Dongyang, Zhejiang Province, the company leverages the Group’s over 20 years of manufacturing experience and complete industrial chain resources to supply safe, efficient and intelligent energy storage products as well as one-stop energy solutions for customers worldwide.
The company’s production base in Dongyang, Zhejiang covers an area of 26.6 mu. It houses modern intelligent workshops equipped with automated production equipment, advanced testing laboratories and a comprehensive quality management system. Standardized management is implemented throughout the production process. Every procedure, from raw material procurement, SMT mounting, PACK assembly and system integration to finished product testing, is carried out in strict accordance with international quality standards, ensuring outstanding safety, stability and reliability of every product set.
Backed by the robust manufacturing capacity of Kingway Group, the company has established a nationwide industrial layout. R&D centers and production bases are located in Chenzhou and Changsha of Hunan, Dongguan and Foshan of Guangdong, as well as Dongyang of Zhejiang. An integrated operation system covering R&D & design, intelligent manufacturing, supply chain management, and global sales & services has been built, enabling stable and efficient product delivery to clients across the globe.
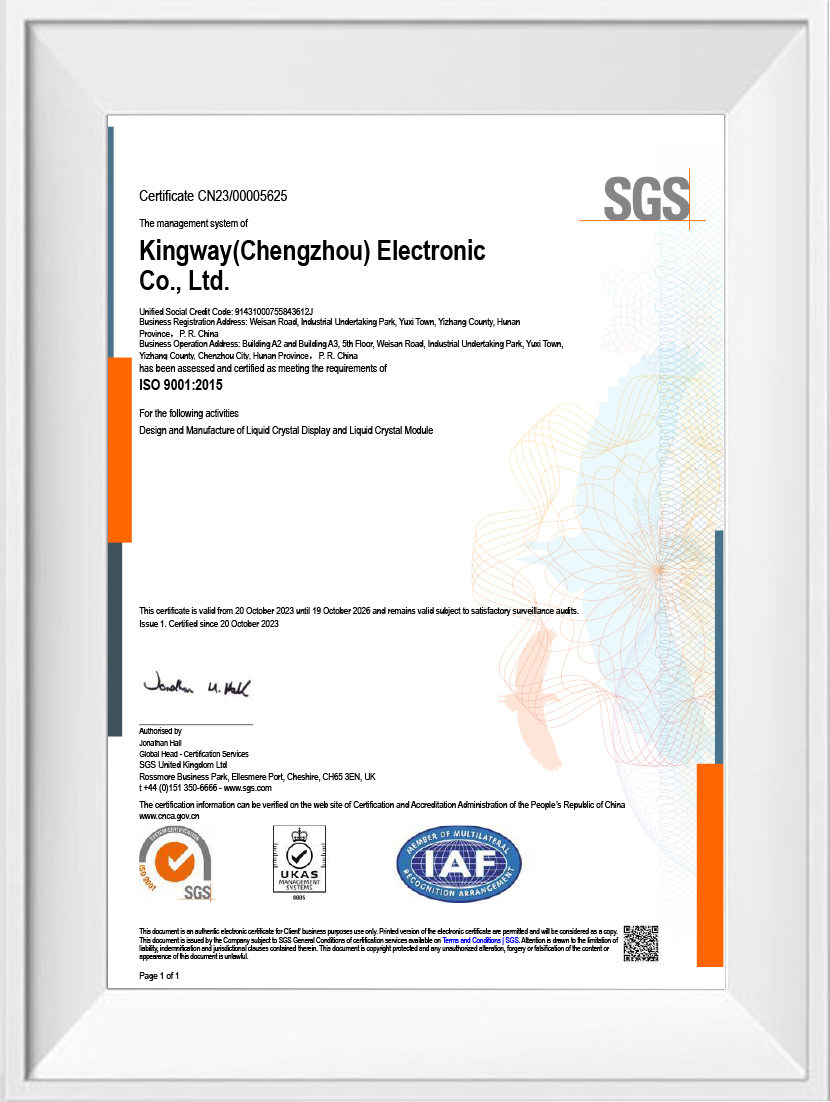
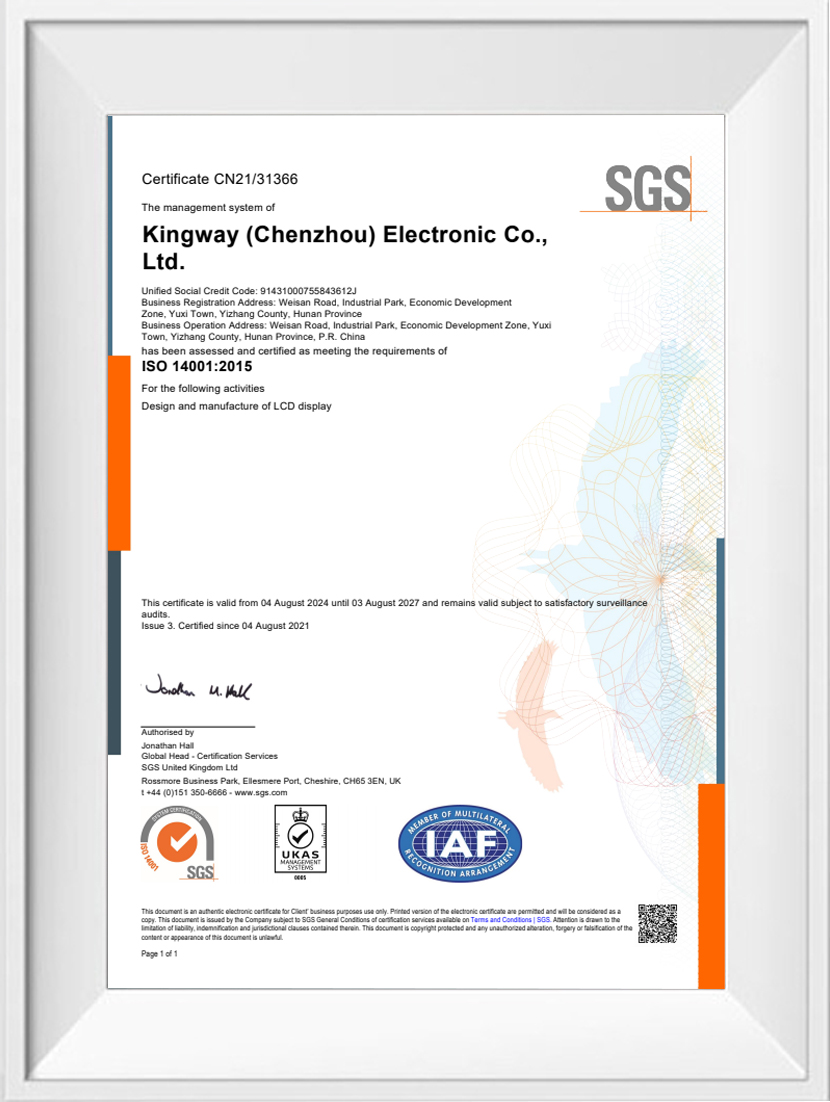
Certificate Of Honor
OUR NEWS
View More
Pay Attention To Our Latest News and Exhibitions
Message Feedback
We maintain deep long-term partnerships with leading global PV inverter brands. Our batteries feature fully compatible communication protocols, delivering customized one-stop PV & energy storage solutions globally.
Ready to Begin?
Quick Links
Product Categories
Contact Information
-
 Email: coopdy@vip.163.com
-
 Phone: +86-19957970189
-
 Address: No. 151 Guanshan North Road, Jiangbei Subdistrict, Dongyang City, Jinhua City, Zhejiang Province, P.R.China
Copyright © Kingway(Jinhua) Display Co., Ltd. Rights Reserved.