EN
 English
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
Rack Mounted Battery ·
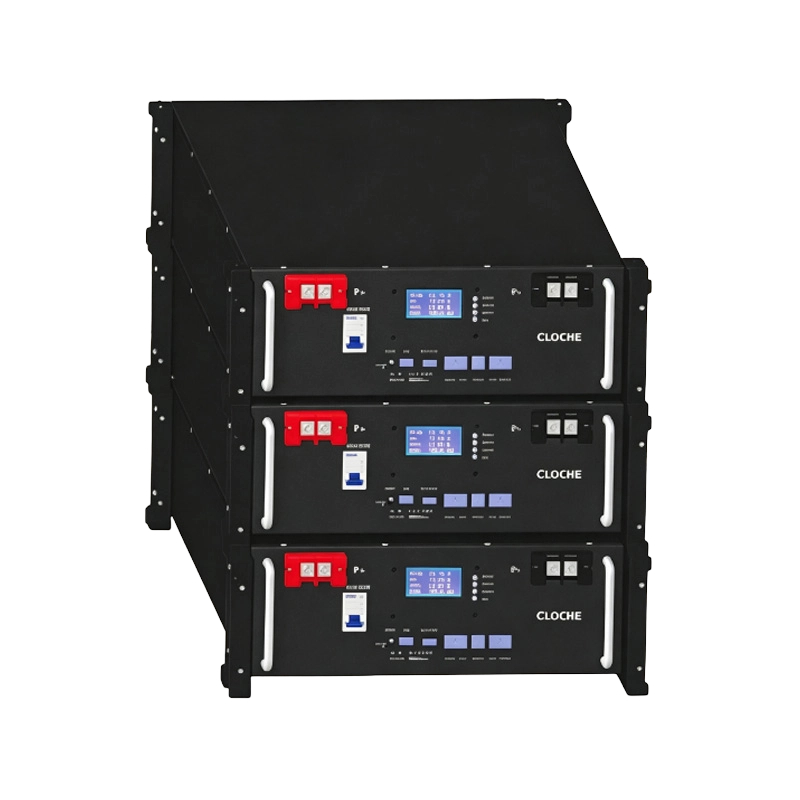
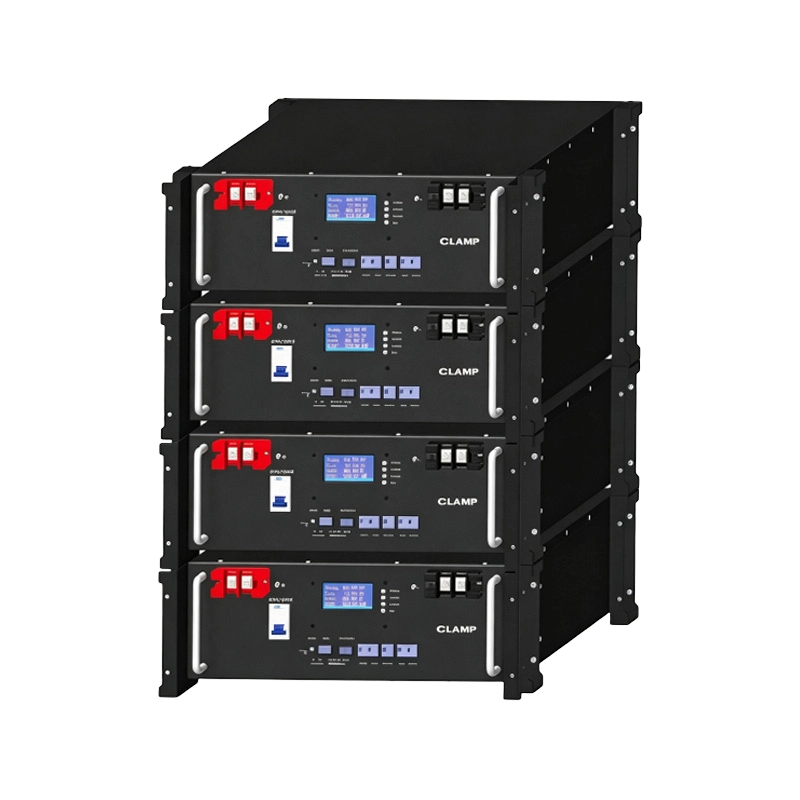
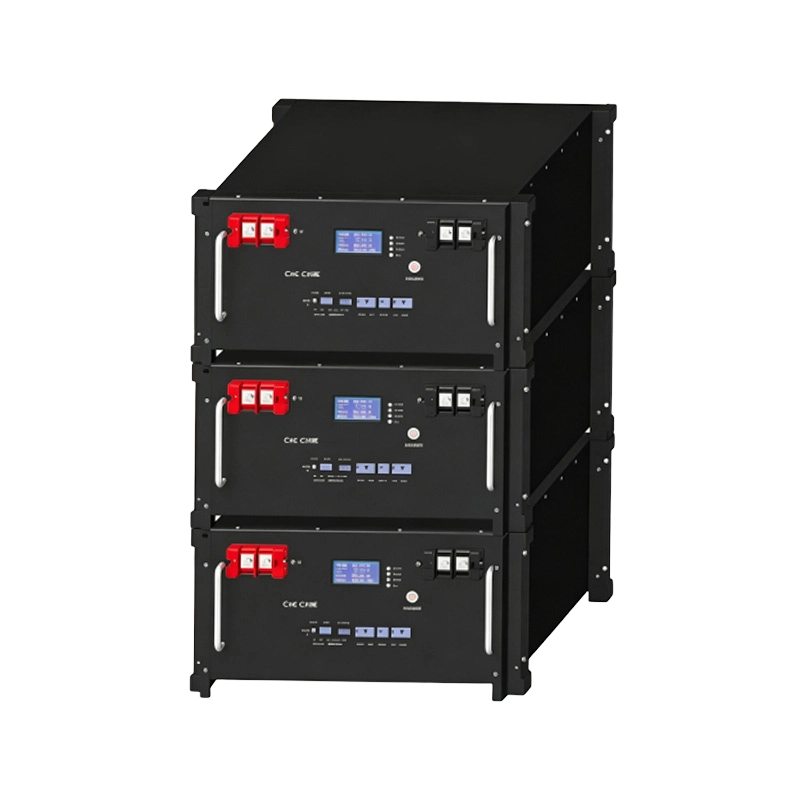
10.24KWh 51.2V 200Ah Rack Mounted Battery
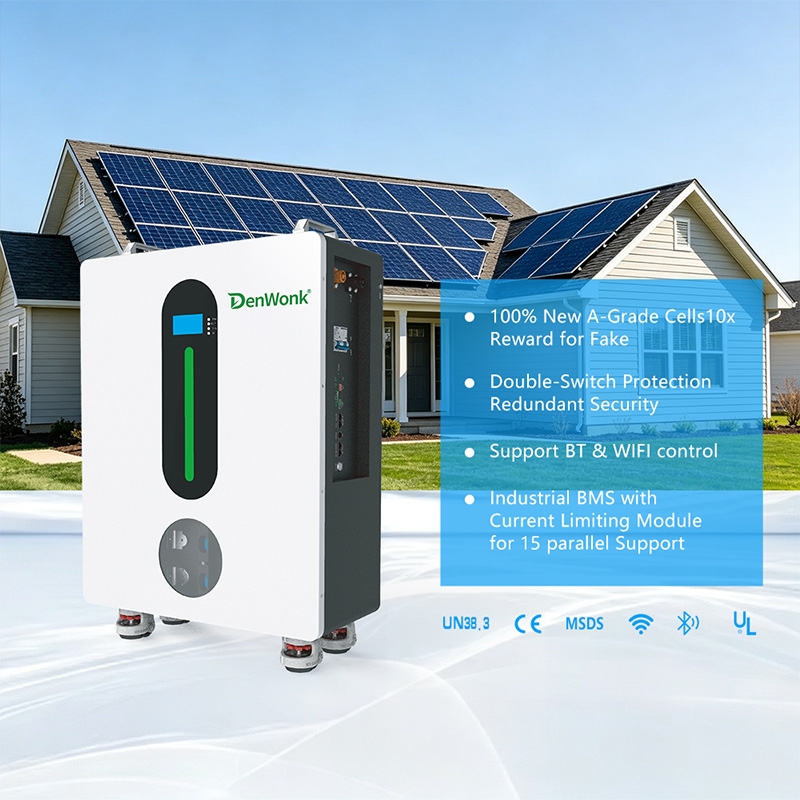
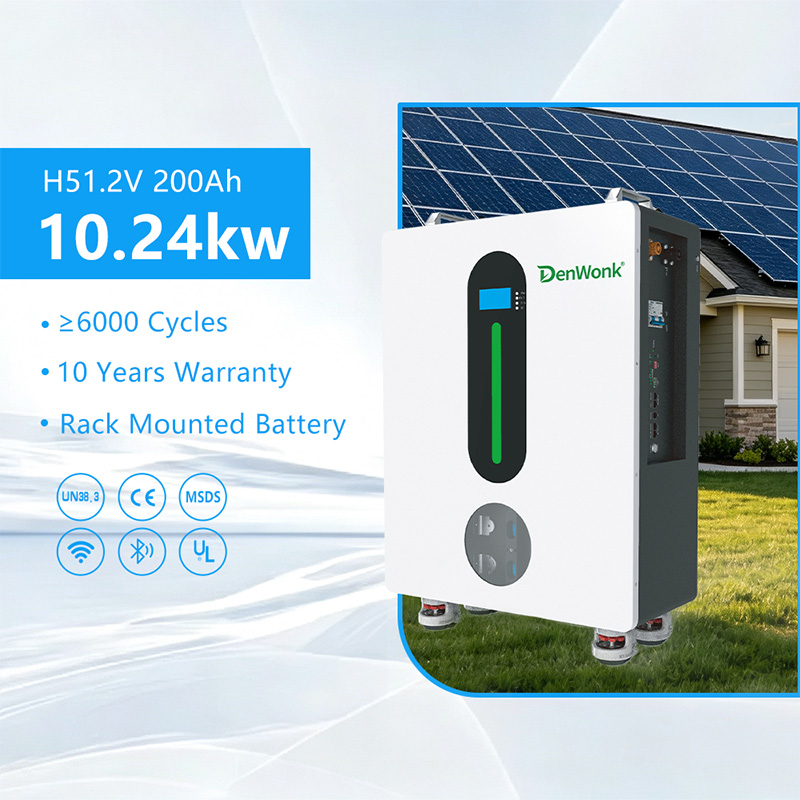
10.24 kWh 51.2 V 200 Ah Rack Mounted Battery is a high-capacity, intelligent energy storage solution engineered for demanding commercial and industrial applications.
Core Advantages:
1. Superior Safety and Unmatched Longevity:
Utilizing robust LiFePO4 chemistry, this Rack Mounted Battery guarantees chemical stability and inherent fire-safety. It offers an outstanding cycle life of ≥4500 cycles at 100% DOD and ≥6000 cycles at 90% DOD, ensuring a lifespan of over 10 years. This significantly lowers long-term replacement costs and provides exceptional Return on Investment (ROI) for any energy infrastructure.
2. Massive Scalability and Intelligent Monitoring:
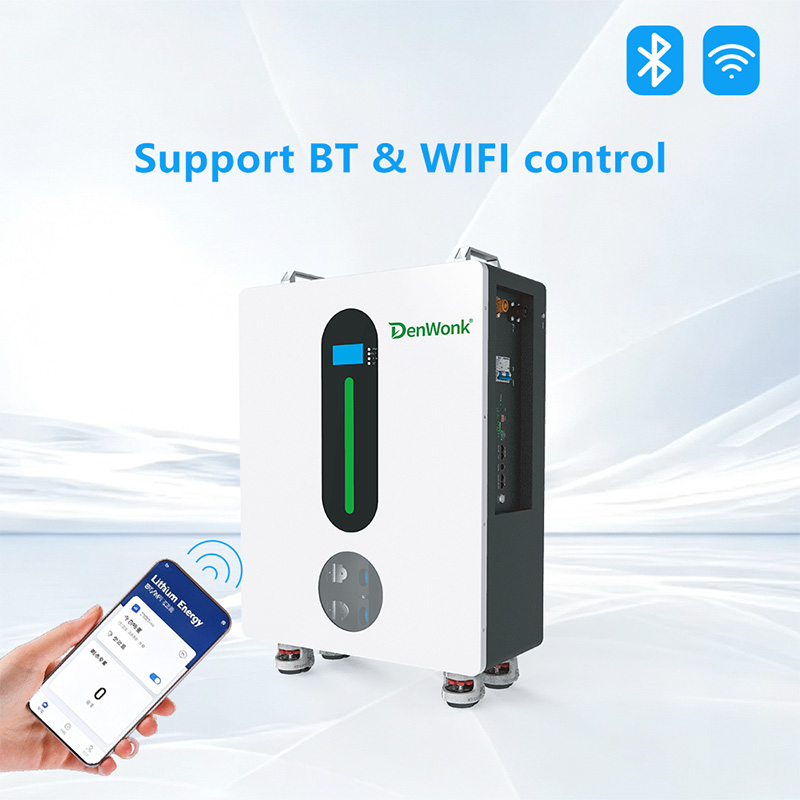
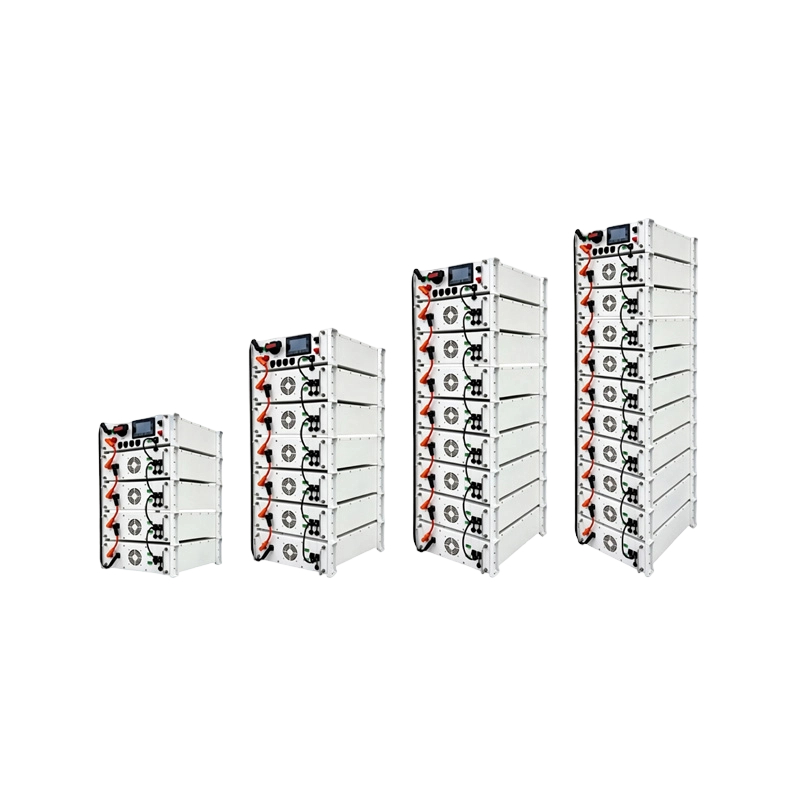
The 51.2V 200Ah Battery features a highly advanced BMS with standard CAN 2.0 and RS485 interfaces, complemented by built-in Bluetooth and WiFi for real-time remote monitoring. Supporting Max.15pcs in parallel (up to 153.6KWh), this modular system seamlessly scales from a large home backup to a comprehensive commercial microgrid energy hub.
3. High Efficiency with Rapid Charging:
Maintaining a continuous 100A charge and discharge current, this 10.24KWh Rack Mounted Battery supports quick energy replenishment and stable high-power output for heavy loads. Its 80% recommended DOD maximizes usable energy capacity while protecting the battery core.
4. Standardized Design for Rapid Deployment:
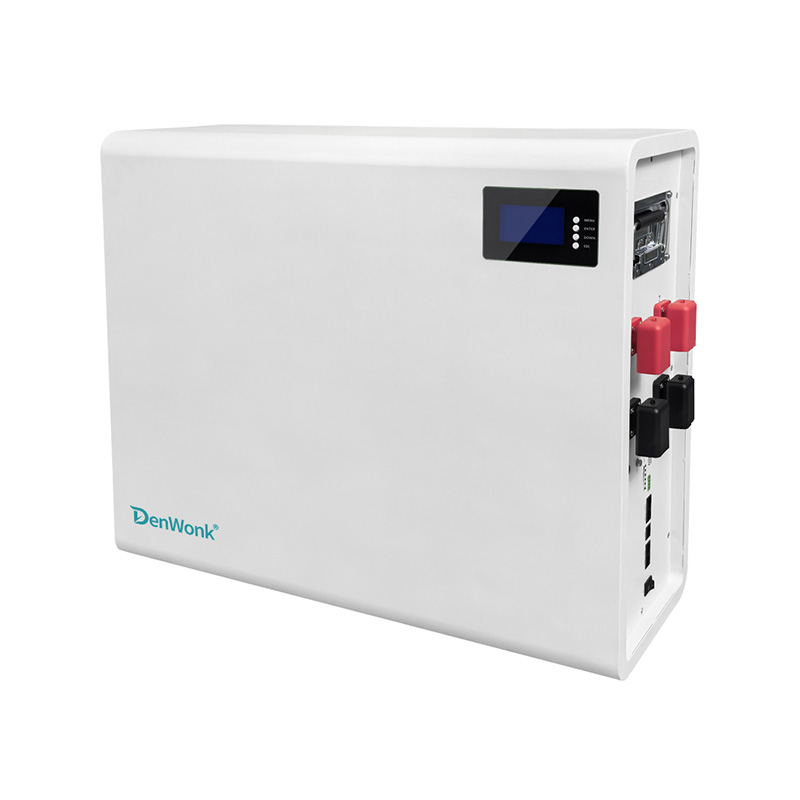
Designed in a standard 19-inch rack-mounted cabinet format (dimensions 800*442*155mm), it utilizes existing rack infrastructure to save floor space. The unit is engineered to operate reliably in harsh environments, supporting a discharge temperature range of -20°C to 55°C.
Product Parameters
Application Scenarios
OEM/ODM Services
Solutions
FAQ
| Main Parameter | |
| Model | LC-LR51200 |
| Battery Chemistry | LiFePO4 |
| Capacity(Ah) | 200 |
| Scalability | Max.15pcs in parallel(153.6KWh) |
| Nominal Voltage (V) | 51.2 |
| Operating Voltage(V) | 46-56 |
| Energy (kWh) | 10.24 |
| Charge Current (A) | 100 |
| Discharge Current (A) | 100 |
| Other Parameter | |
| Recommended Depth of Discharge | 80% |
| Dimension(LW/H,mm) | 800*442*155 |
| Weight Approximate(kg) | 85 |
| MasterLED indicator | 6LED(SOC:0~100%) |
| 3LED(Power on,working, alarming) | |
| IP Rating of enclosure | IP20 |
| WorkingTemperature | Charge:0°C~55°C Discharge:-20°C~55°C |
| Storage Temperature | -30°C~60°C(humidity ≤75%ROH) |
| Humidity | 5%~95% |
| Altitude | ≤2000m |
| Cycle Life | ≥4500 cycles (25+2°C,100%DOD,80%EOL) |
| ≥6000 cycles (25+2°C,90%DOD,70%EOL) | |
| Installation | 19-inch standard cabinet, cabinet depth >1100mm /with rack |
| Communication Port | CAN2.0, RS485 |
| Wireless Communication | Bluetooth, WIFI |
| Warranty Period | 5 years |
| Certification | CE-EMC.MSDS.UN38.3 |
The 10.24 kWh 51.2 V 200 Ah Rack-Mounted Battery is widely deployed across various sectors:
Commercial & Industrial ESS: Large-scale solar storage, peak shaving, and valley filling systems.
Telecom & Data Centers: Base station backup power and UPS systems for critical IT infrastructure.
Microgrids: Community-level energy storage and emergency power supply systems.
Residential ESS: High-energy backup for large villas and off-grid homes.
We provide comprehensive OEM/ODM services for global wholesalers and system integrators:
Custom Manufacturing: We produce rack-mounted battery systems tailored to your specific voltage, capacity, or BMS protocols.
Branding & Packaging: Customized logos, labels, and environmentally friendly packaging to fit your brand identity.
Technical Support: Provide in-depth technical drawings, communication protocol integration, and custom firmware development.
Fast Sampling: Rapid prototype development and sample delivery to accelerate your market penetration.
1. System Integrators
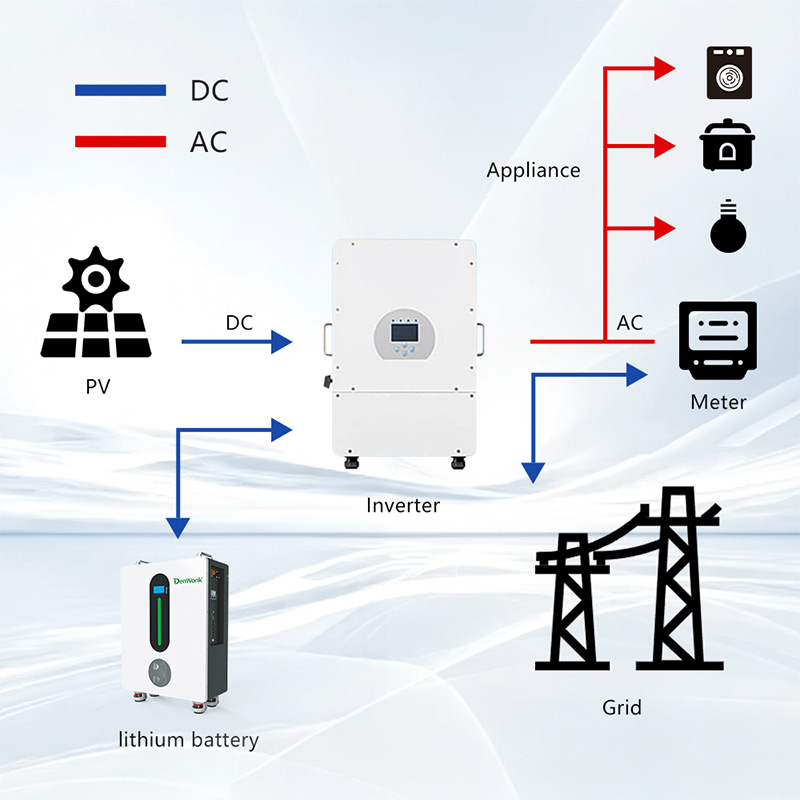
Modular battery packs supporting up to 15 units in parallel (153.6KWh), perfectly compatible with mainstream inverters.
2. Data Center Operators
Standard 19-inch rack units that seamlessly fit into existing server racks for reliable backup power.
3. EPC Contractors
Industrial-scale solutions offering high cycle life (≥6000 cycles) with a 5-year warranty, ensuring low Levelized Cost of Energy (LCOE) and high project ROI.
4. Brand Owners & Wholesalers
Full OEM/ODM customization support, including branding, interface adjustments, and WiFi/Bluetooth monitoring features tailored to local markets.
Q1: The 10.24KWh 51.2V 200Ah Rack Mounted Battery is engineered with a 5-year warranty and advanced LiFePO4 chemistry, what specific benefits does it offer?
The 10.24KWh 51.2V 200Ah Rack Mounted Battery offers superior safety, a lifespan of over 10 years (≥6000 cycles at 90% DOD), and massive scalability (up to 153.6KWh). Its intelligent BMS supports real-time monitoring, ensuring long-term reliability and lower TCO.
Q2: How long is the production lead time?
The standard production cycle is 15 to 20 days after order confirmation and deposit payment. We can expedite production for urgent large-scale projects.
Q3: Can you provide free samples?
Yes, we can provide samples for quality testing. We offer free sample pieces; however, the courier/shipping cost is usually borne by the buyer, which will be refunded upon placing a bulk order.
Q4: How does the battery expand in parallel?
This Rack Mounted Battery supports a maximum of 15 units connected in parallel, achieving a massive total energy capacity of 153.6KWh without the need for external controllers.
Q5: Do you offer customized communication protocols?
Yes, we provide standard CAN 2.0, RS485, Bluetooth, and WiFi. We also offer OEM/ODM services to adjust communication parameters to perfectly match your specific inverter or EMS system.
-
0 m²
Land Area
-
0+
Industry Experience
-
0+
Number of Employees
OUR STORY
Become a World-Class Green Energy Enterprise, Build Low-Carbon Future
Kingway(Jinhua) Display Co., Ltd., a subsidiary of Kingway Group, is a high-tech enterprise focusing on the R&D, manufacturing, sales, and solution provision of new energy storage products. Headquartered in Dongyang, Zhejiang Province, the company leverages the Group’s over 20 years of manufacturing experience and complete industrial chain resources to supply safe, efficient and intelligent energy storage products as well as one-stop energy solutions for customers worldwide.
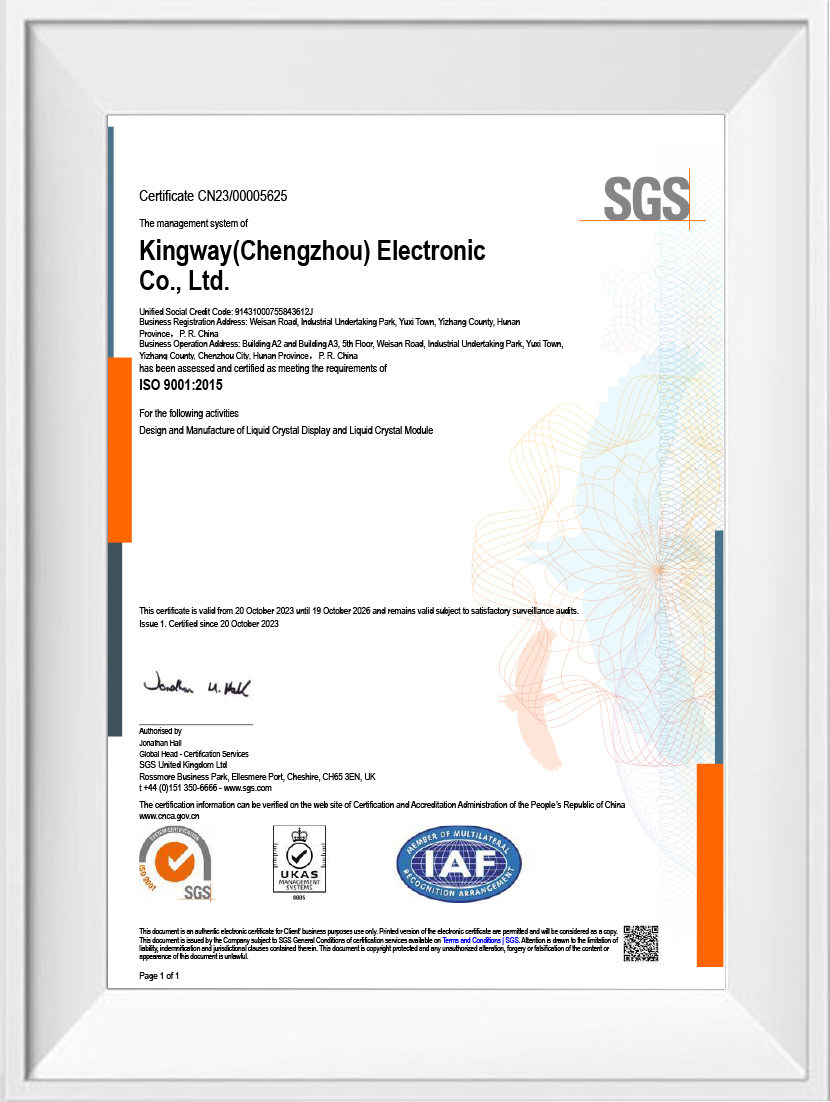
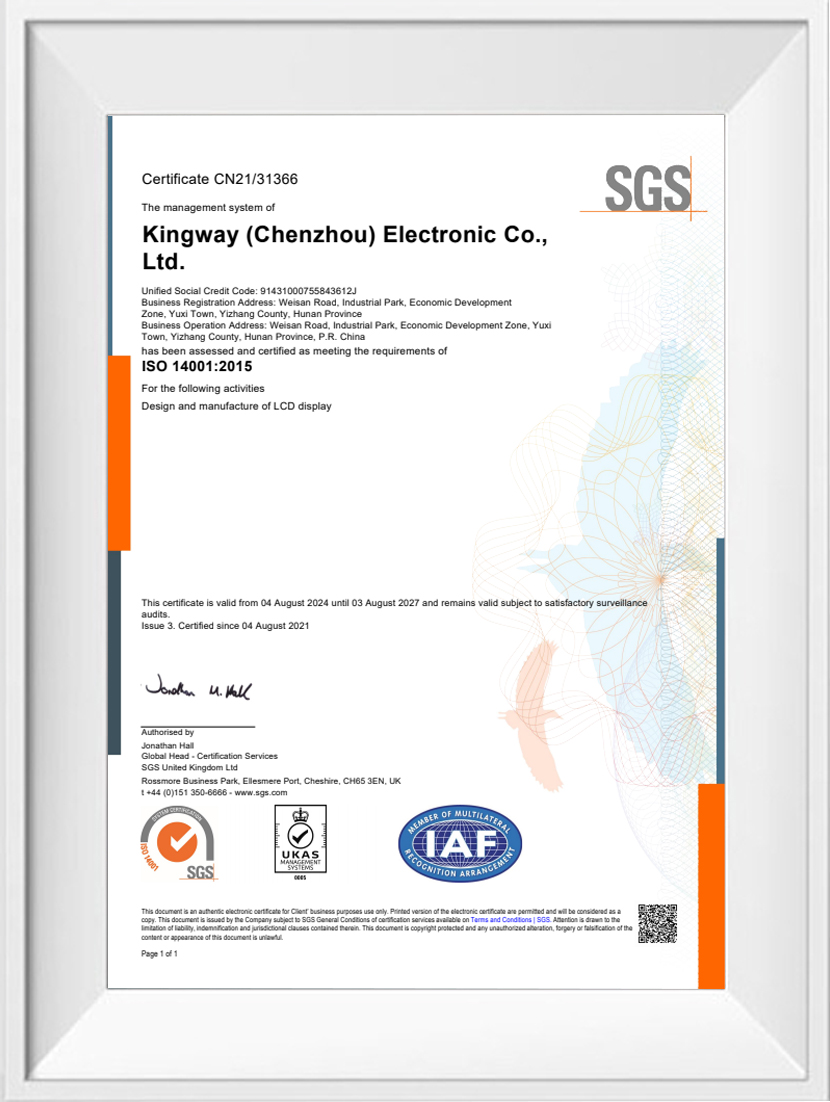
The company’s production base in Dongyang, Zhejiang covers an area of 26.6 mu. It houses modern intelligent workshops equipped with automated production equipment, advanced testing laboratories and a comprehensive quality management system. Standardized management is implemented throughout the production process. Every procedure, from raw material procurement, SMT mounting, PACK assembly and system integration to finished product testing, is carried out in strict accordance with international quality standards, ensuring outstanding safety, stability and reliability of every product set.
Backed by the robust manufacturing capacity of Kingway Group, the company has established a nationwide industrial layout. R&D centers and production bases are located in Chenzhou and Changsha of Hunan, Dongguan and Foshan of Guangdong, as well as Dongyang of Zhejiang. An integrated operation system covering R&D & design, intelligent manufacturing, supply chain management, and global sales & services has been built, enabling stable and efficient product delivery to clients across the globe.
Certificate Of Honor
OUR NEWS
View More
Pay Attention To Our Latest News and Exhibitions
Message Feedback
We maintain deep long-term partnerships with leading global PV inverter brands. Our batteries feature fully compatible communication protocols, delivering customized one-stop PV & energy storage solutions globally.
Ready to Begin?
Quick Links
Product Categories
Contact Information
-
 Email: coopdy@vip.163.com
-
 Phone: +86-19957970189
-
 Address: No. 151 Guanshan North Road, Jiangbei Subdistrict, Dongyang City, Jinhua City, Zhejiang Province, P.R.China
Copyright © Kingway(Jinhua) Display Co., Ltd. Rights Reserved.